Monday, December 31, 2012

Lean Thinking - Respect For People

The foundation for Lean Transformation

Beginning the Journey and navigating this unknown (but common sense?) path requires a change in how Leaders and Managers relate with the employees.  This will be more than having a banner that states "Employees Are Our Most Important Assets!" in a 72 pt font or some kind of Employee Involvement committee that meets once a quarter whether they need to or not.  This is going to require you putting on your shoes and going to the place where the work happens.  And this should not be a one-time event, schedule the visits if you need to between your triple-booked meetings.

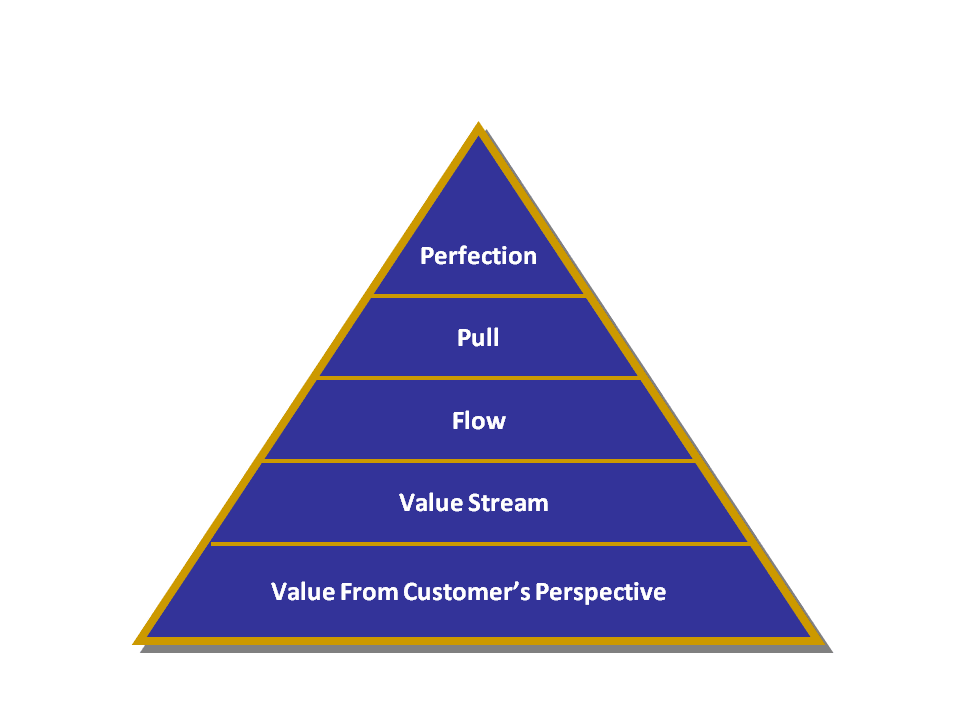
House of Lean with Respect for People as foundation
If this is your first time for your employees to see you on the floor, there may some staring and pointing, or some may even introduce themselves to you.  But I'm sure in this day of enlightened management techniques, you will not experience anything like this... right.  Employees will be open and honest if they are familiar with you and have some type of positive rapport.

You can also attend some of the team's meetings, listen to the comments they are making.  When was the last time you shared the company's strategy with them?  Do they make plans that align their Goals & Objectives with the direction of the company?  Do they understand how this Journey helps to improve the company's stability and long-term success?  Have you ever met anyone on the Board?  This Respect and Communication moves up and down the Leadership Chain.  Communication is not just Leadership making commands and the employees executing their wishes.

When we are developing and using our listening skills, we need to capture those comments that illustrate potential road-blocks to the implementation of the strategy.  These comments will need to be corroborated with your staff and seen in action.  The employees are looking for help when they need it, but we don't instantly implement suggestions just because they come from "the floor".  You will need to validate the problem's existence with measures.

We're not trying to make this a 12 month long six sigma project, sometimes the root causes are standing there and taunting us to make the first move.  Involve the Smart People in the measures, root cause identification and determining the solution.  The entire team owns the problem and the solution, this ownership will help facilitate the long-term solution that is followed and maintained.  Whatever the solution that is implemented, make certain that it is reflected in the standard work instructions.

When you have a measurable difference in the two methods, it's time celebrate success with the team.  Order some pizzas, make some certificates of appreciation, get them some gift cards, maybe it's time for a promotion, or some sort of positive reinforcement of the message that we are together on the Journey.  One instance of problem-solving does not make someone Lean, nor does it solve all the problems so someone "gets a belt".

If the problem is not validated, talk with the person who thinks it is there.  You may have missed something important, it may not align to the strategy, or there may be a deeper conversation to be had.  It is entirely possible that the Good Idea Fairy has been in the area having her way with unsuspecting employees.  Ideas have to be connected to a measured and validated problem statement.  If the decision is to not do anything about the problem yet, let the employees know why and when it may be addressed.

Improving is difficult enough, but having the team on board can make the Journey smoother.  Open and Honest communication can help make it happen.

Tuesday, December 25, 2012

Merry Christmas 2012!

Today is a good day to be with family and friends, and see if you can follow the Standard Work provided with many of the toys you may be constructing today.  The good one will have pictures to show what "right" looks like.  These are good examples to use around the office while you are creating or updating your own SOPs or Desk Guides.


Merry Christmas to all my friends and followers!  I hear that the Time of Resolutions is just around the corner!

Monday, December 17, 2012

When Is Enough, Enough?

A Long Time Ago In A Galaxy Far, Far Away...   

I was teaching the Statistical Process Control & Capability module during a Lean six sigma Green Belt class and one of the students asked, and I'm going to paraphrase, "When is enough, enough?"  I think this would be a normal question to ask while learning how to Make Value Flow.  The question came from one of my Quality friends, and I'm sure he was thinking about all the different processes he supported that needed improvement and certainly not when he could put his feet in the air and his "you-know-what" in the chair.

If you have been measuring your performance, then you should have some amount of data collected around the problem you are experiencing.  If you are having quality problems, you may have Defects Per Unit (DPU), or Defects Per Million Opportunities (DPMO).  If you are having delivery problems, you may have Cycle Time or Number of Days Early/Late.  If you are having cost problems, you may have Cost Per Unit or Weekly Printing Costs.  Either way, you need some data that represents your process.


We can see the performance is in control and the stable, but is the process meeting the customer's needs?  This is always the right question!

When we use SPC we are looking for  indicators that signify when to start asking questions about the process.  There are four that are the easiest to use and remember; 1) Any points outside of the control limits, 2) Six points consecutively going up or down, 3) Nine point consecutively above or below the center, and 4) 14 points consecutively going up and down.  Having a process that performs within these four parameters means that our process is in control and stable, which indicates the flow is predictable.

Here is your SPC warning!  Do not let any of you Quality Engineers catch you putting specification lines on your SPC chart.

What it does not tell us is are we meeting customer expectations.  This is where we take our Voice of the Customer specifications and lay them on top of a histogram of the data.  From here we can see our performance compared to customer specs of no more than 21 days (USL, LSL).

Current State

And as we can see from the fine specimen above, when our cycle times are 22-25 days we are not meeting customer expectations.  Our process is in control, but not performing to the wants and desires of the customer.  In fact it may be possible that our favorite customer is looking for a new supplier of their information needs as we speak and I think that immediate action is required.

At this point you should be constructing a charter, assigning one of your belts to lead the project, and kick-off the team.  Work your best as a Project Sponsor, Smart Person or Supplier/Customer and document the results in an A3.  When you have enough data with the new process you can see how the center and spread fit within the specifications.

If you have identified the root causes and adequately implemented a new process that has improved flow, then you are done with that process for now.  The biggest indicator is the edge of the distribution is some amount away from the specification.  For you math nerds, below is the formula and you want to get as close to 1.5 as you can.


Improved Process #1

Based on our results we can see that are delivering everything on time, and if we finish early we can hold the deliverable until the customer is ready.  Be wary of producing too much too fast.  That would make our work-in-process increase, which means the window between "doing work" and "getting paid" increases and this is detrimental to cash flow.

At the end of the day we want our products to flow without stopping though our value-added operations to meet customer demand.  Deliver too late and the customer must wait (Wait Time), but if we deliver too early the customer has to over-handle (Excess Processing) the product until they are ready to use it and this is "Inventory" they have to hold until they are paid.  If you have paid any attention over the last 5 years, this over-capitalization is one of the causes of the downfall of the American automobile industry.  Leadership is the decision-maker, but the following histogram represents one possible best fit.

Improved Process #2
Improving performance is not something that will automatically happen, learning curves are not absolute.  Market forces fluctuate and your ability to adjust with them could be one of your long-term indicators of success.

How do you use your data for improving flow?

Monday, December 3, 2012

Designing the Perfect Process

In all the work places we have been, do you remember ever asking how someone came up with this insane method to respond to a customer order?  Taking the order is easy, we receive an email from our website catalog system.  But everything else we do after that resembles a group of 5 year old Americans playing futbol (ok fine, soccer).

We would like to think the process was designed using the smartest people, using the best tools, and the most responsive and fair management techniques taught in the best MBA schools.  No such luck my friend.  Your current process was haphazardly put together using years of bad results from battling against lawyers, the least amount of communication possible, and it's certainly not documented or repeatable.  The last thing we also want is someone able to measure the process only to beat us up with the charts.


Does any of this sound familiar?

When do we start creating the new process?  The best situation would be during New Product Development or when you start to go after new customers.  Sometimes your current process does not meet the customer needs and small step improvement is not enough.

Let's start by defining a few characteristics of the perfect process and what it looks like:

1)  It has no review cycles, quality comes from the process
2)  There is no guessing
3)  There is no hunting and gathering
4)  The time from order to fulfillment is as short as possible
5)  The customer receives the order defect free and exactly when they want it

With this in mind, let's start....

You will need to collect any regulations that may impact your process or product, voice of the customer using surveys or direct interviews, and any business concerns that may exist.  We will put this on a House of Quality or Quality Function Deployment (QFD) (same thing... mostly, just don't say that to one of the Six Sigma guys).  Rate, prioritize, and score these to help determine the level of focus to be applied during the actual design of the flow.

Benchmark other organizations or companies dealing with the same type of product.  Be open and honest, those organizations getting good results will be very proud of their process and will happily show you their stuff.  There may be more information published on the internet, in trade magazines, or state/federal government survey data.

More time is used defining requirements so when it is time to document the new flow it almost creates itself.  Ok it's not that easy, you will need the smart people to help lay out the steps.  Lock everyone in a room, tape a long piece of butcher paper on the wall, break out the sharpies and sticky notes, and tell everyone to put their shoes on 'cause they're going to go do some work.

Start with the first signaling step and have the rest of the team fill out the remaining steps of the flow.  Keep a large copy of the QFD taped to the wall next to the flow so they don't forget about the customer's and other process stakeholder's needs.  Add the inputs and outputs to each step step to help the team focus on the thing going through the system.  Complete your Value Analysis and look for any of the 8-Wastes that can be eliminated before the process goes live.

When you have this completed and the team reaches consensus on the flow, put it in your SOP or Deskguide format.  Create the training to deploy the new process to the other team members who have not seen it and any new team members that come on board later.  Determine the measure points for Quality, Cost, Delivery, and any other Customer measure to finish the process.

If you have some sort of process automation, make sure you have separated the steps in the process to show which are performed by people and those performed by the computers.  Don't mix these as computers can't think critically and make decisions and people should not be creating information that no one will see.

Does the perfect process really exist?  Probably not, but can get very close.  All processes need to have learning steps so when quality or cycle time issues are identified they can be quickly eliminated from the process.  Update the Deskguide and document in an A3.

Everyone raise your right hand and repeat after me.  Go ahead, get that hand in the air.

1)  I will not accept poor quality from my external or internal suppliers.
2)  I will not pass on poor quality to my external or internal customers.

OK, put you hand down and share cool things your have seen in your processes!

Thursday, November 22, 2012

Giving Thanks!

This time of the year we offer thanks to those people or things we have experienced through the year.  The lists are always long and we sometimes leave one or two off.  The great thing about thanking someone is that you don't have to wait until the third week of November to do it.

Beautiful Oklahoma Sunrise

And since we are here, I want to thank you for dropping by to read my latest ramblings-on about Lean Transformation and how we as Leaders fit into the puzzle.  I hope you continue to visit and leave comments because the conversations add depth to the concepts.

Monday, November 19, 2012

We Just Lost Half of the Team

One day were are a happy team, plenty of work coming in and we don't have too many customers calling every other day about their orders.  Then the boss from corporate comes in, goes to our branch manager's office and closes the door.  This does not look good.

A couple of the sales guys split, muttering something about hand delivering some reports.  A few of us go to lunch and the rest plan out the remainder of the day.  The manager's office is empty when we return, but our in-boxes have a meeting notice at the end of the day.  Of course we all panic, there was nothing in the body of the email and we never have cake at the end of the day.

The remaining minutes and hours count down and we all meet in the larger conference room.  The branch manager is standing at the front of the room with a powerpoint on the wall.  He goes through the charts; sales per employee, backorders by customers, quality surveys from customers, accounts past due to suppliers.  None of this looks good and our question was how long had it been like this?  Has anyone been paying attention?

One by one we were called into the office.  There were three of us at the table, the branch manager, someone from corporate HR, and I.  They asked if I understood the information presented and I said that I did, and I asked how long has performance been like this?  He made some comments about the softness of the local economy and expected it to turn around at any time.  None of what he said sounded good.

About half the team survived this round of layoffs.  We had to do something.....

This is how some organizations start their Lean Journey.  Sometimes we see teams respond with positive change by using their metrics and creating a plan to improve customer satisfaction and aggressively getting new orders and customers.  Sometimes the teams blame others, lobby for a government bail-out, and continue in their same, old, wasteful ways.

Just like any other personally damaging situations; smoking, obesity, and high-stress are all responses to bad practices and our businesses can exhibit the same types of response factors.  Fire-fighting, low customer satisfaction, and poor team relationships are not going to fix themselves.  You can't wait for the team to turn around on their own.  Someone (you) needs to make a bold statement.  "We will no longer be in the Fire-Fighting business!"

You will hear some chuckles, but it's ok.  Half of the team is gone, so how do you do the same amount of work with less people?  It's not simple, but you're going to have to learn from your mistakes.  Talk to your customers about your delivery, look at how you do things and improve.  You have to get the team out of Egypt and get Egypt out of the team.

You  may be tempted to start creating plans and roadmaps and start bringing in high-powered consultants.  If you were starting the Lean Journey when times were good, those tools would be perfect, but you are not and we need to start the transformation now.  Your Burning Platform (or BHAG) is right in front of you, take a picture if you need one.  Start with the processes you use to create your products and remember this analysis is based on the thing going through the system or process.  Do you have any performance data; cost, quality, delivery?  If not, then begin collecting it now.

Have you talked to your customers yet?  We will use that information when we create the new processes.  We may even pull out our House of Quality (or QFD) to help align customer needs and the requirements we must comply with.

We then map those processes and remember this is based on how we do it now, not how we want to or what the SOP says how the process is supposed to operate.  Ask where are those inspection review processes and how we fix the documents?  Circle these steps with a Red Sharpie, these will be targeted first!  If you have some sort of review trail from emails or a workflow system, put the quality failures in categories and force rank them by count so you can attack the worst offenders first.

Once you have that, get the team together for a fishbone party.  Remember that you put the problem statement or quality failure at the head of the fish and the potential causes on the four bones.  What four bones?  I'm glad you asked.

If you start using Man, Method, Measurement, Mother Nature, Material, and Machine in the office you will spend the next hours trying to get the team to not think of these in manufacturing terms.  In our information processes we use People, Place, Policy, and Procedures.  Nearly all issues that exist today will fall into those categories.  When the team is passed out on the floor and have nothing else to give, begin weeding out the least likely causes and work your way up to the most likely or direct causes.

Bundle related causes together and begin brainstorming potential solutions.  We will also begin to start mapping out the new process based on the number people available, a "No Fire-Fighting" culture, a bold statement that our internal teams will neither accept or pass on defective information, and we cannot inspect quality into our products as high-quality must come from the process.  Everyone must buy-in to the new process, both the smart people doing the jobs and the Leaders of the organizations.

Once you have tried a few things and have picked the best of the best (for now) you need to document how the process operates so when new team members come on when the economy recovers they have something to be trained on.  Determine some metrics so poor performance is not a surprise anymore and there will be plenty of time to respond.  Everyone needs to know what right looks like.

Transforming under fire is never pleasant, but the good times just doesn't always provide the need for change.  Bad things happen, and then we pick up the pieces and continue on.

When your team has been through a rough time, what kind of lasting change did you make?

Monday, November 12, 2012

Incentivizing Improved Performance

Have a team that produced great results when their past performance was consistently less than stellar?  Was this a one-time bump or will there be long-lasting results?  Do you think the team will show high performing metrics next review?  You probably know the answer to this.

Companies and their internal organization should have plans to improve or innovate their products and services.  Those plans need to be developed with and approved by the Board, flowed down through the Leadership Team, and marketed to the employees.  These plans should be visual, achievable and relevant enough so that anyone we ask will understand what right looks like.  We are asking for everyone's support as if the future of the company depends on it, because it does.

We know this is a journey and we should be plotting our course, stop once in a while and take a look at the progress you have made.  Bring the team together and show them that working together to a common goal can make happen. Along the way, take pictures, shoot some video, interview people involved in the change, and use your project documentation to create storyboards to help show the transformation.  Remember this is not small step change on one little project, but transformation across an entire site.


Think about how to reward the teams for this amount of change.  A pay increase would be great, but we're talking about real employee appreciation not short-term impacts that are quickly accepted as the normal condition.  Employees today are looking to make a personal connection that can act as compound interest on their careers.  They also want to know that their contributions are making a difference.

Companies in the recent past paid some percentage of the savings.  This is nice too, but too often the savings are soft or cost avoidance types of savings.  While these opportunities need to be implemented also, they increase capacity of the team and have the affect of reducing over-time to achieve better balance between life and work.  We have seen this types of reward systems become abused and leaves a bitter taste with the Leadership team when reductions to bottom line costs are not realized.

This type of thinking can certainly be used to motivate employees to continue improving and innovating, and employees knowing their efforts are appreciated make huge steps in retaining them.  Green Belt or Black Belt shirts with company logos are nice, but mentoring from the boss and opportunities to move up the ladder reinforce the confidence in the actual people doing the actual work.

What type of actions have you used to show employee appreciation?